Meaning
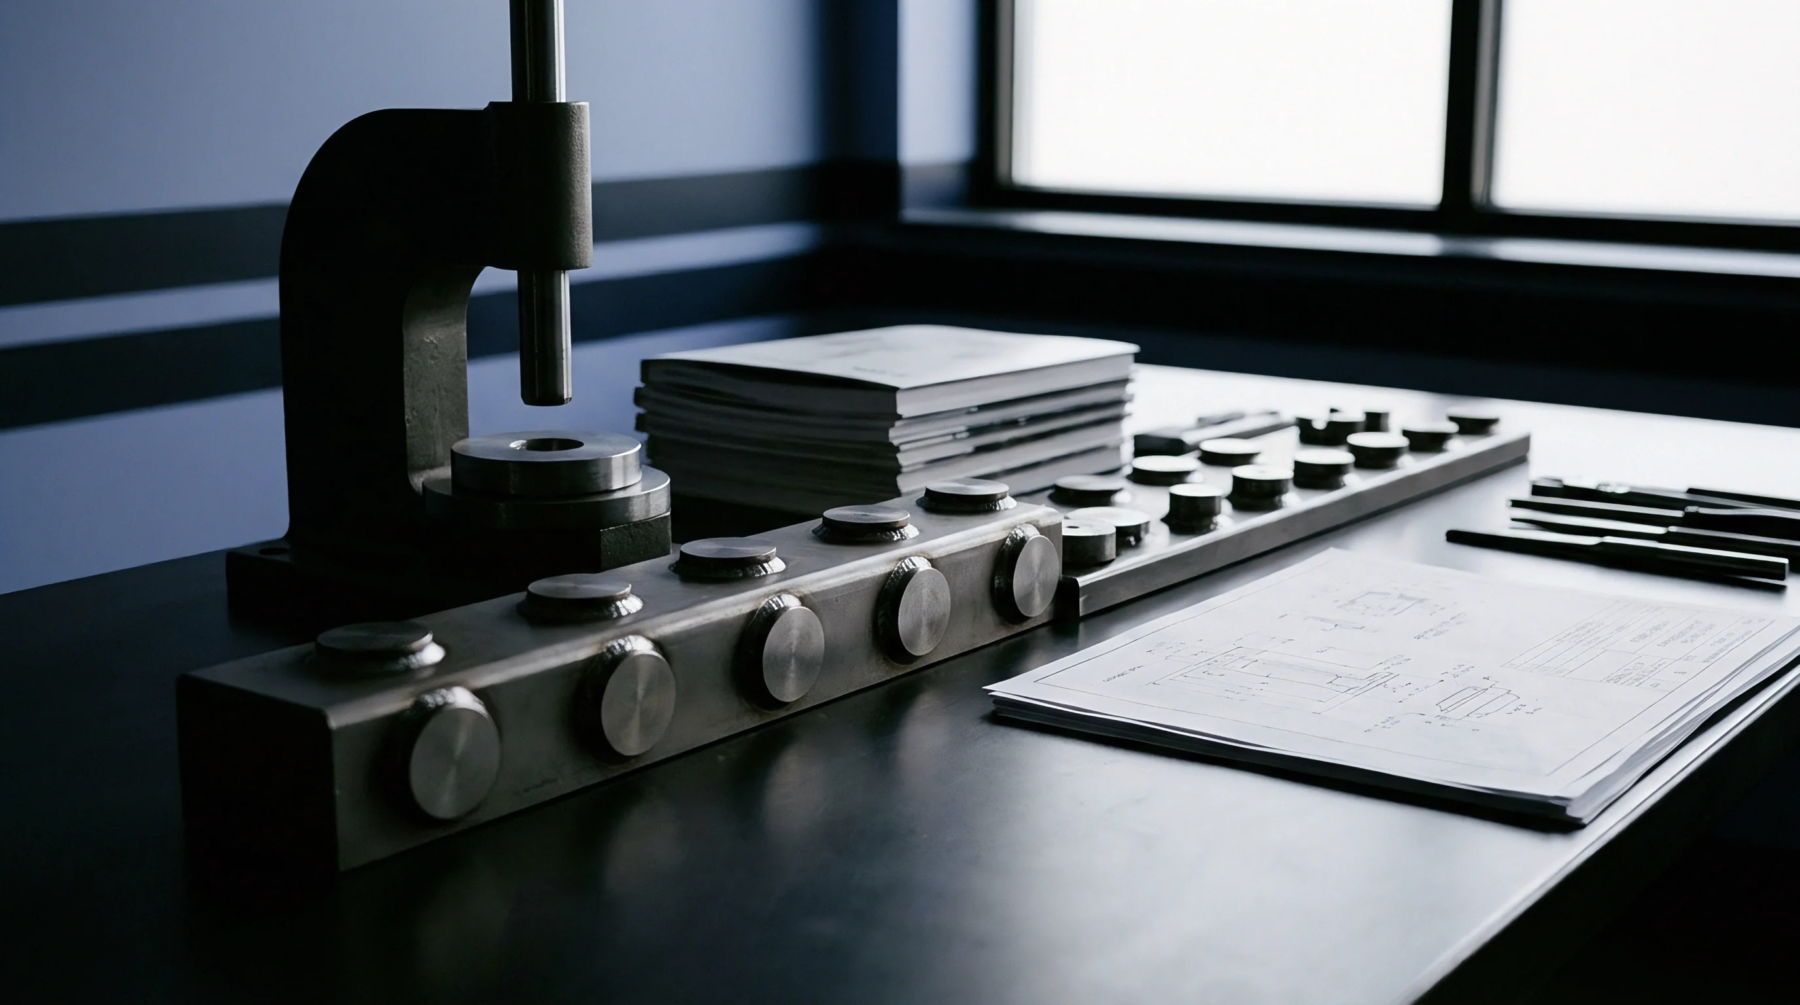
Mechanical stamping clearances measure the vertical distance from the top of the press bed to the bottom of the slide when the stroke rests at bottom dead center with the adjustment all the way up. Tooling designers verify press shut height to ensure production stamping dies fit safely within the working envelope of selected manufacturing equipment. The dimension ceases to apply to open-gap horn presses or unrestricted hydraulic presses lacking a fixed mechanical crank stop.
Tooling Compatibility
Stamping dies must match the rated clearance envelope of the stamping machine to prevent catastrophic interference or incomplete die closure. If tooling height exceeds available press shut height, upper die shoes collide with the ram, damaging expensive guideways and cracking press frames. In pressroom scale-up audits, technicians measure bolster plate thickness to establish true working daylight before mounting multi-station progressive dies.
Adjusting the motor-driven slide mechanism aligns die shut height precisely with machine stroke parameters.
Defect Prevention
Insufficient stroke penetration produces incomplete part coining, inaccurate bend radii and severe dimensional variation across deep-drawn stampings. Excessive shut height compression overloads tonnage monitors, fracturing die pins and generating excessive vibration throughout the machine base. Demonstrated production yield depends on holding shut height repeatable under full thermal operating equilibrium.
Stroke Boundary
Thermal expansion of the press frame during continuous high-speed cycling alters the actual operational clearance by fractions of a millimeter. When high-tonnage stamping generates significant heat, press shut height decreases slightly, increasing part coining pressure unless monitored by automatic shut height compensation systems. Mechanical clearance definitions remain reliable only when quoted alongside specific bolster configurations and slide adjustment limits.