Meaning
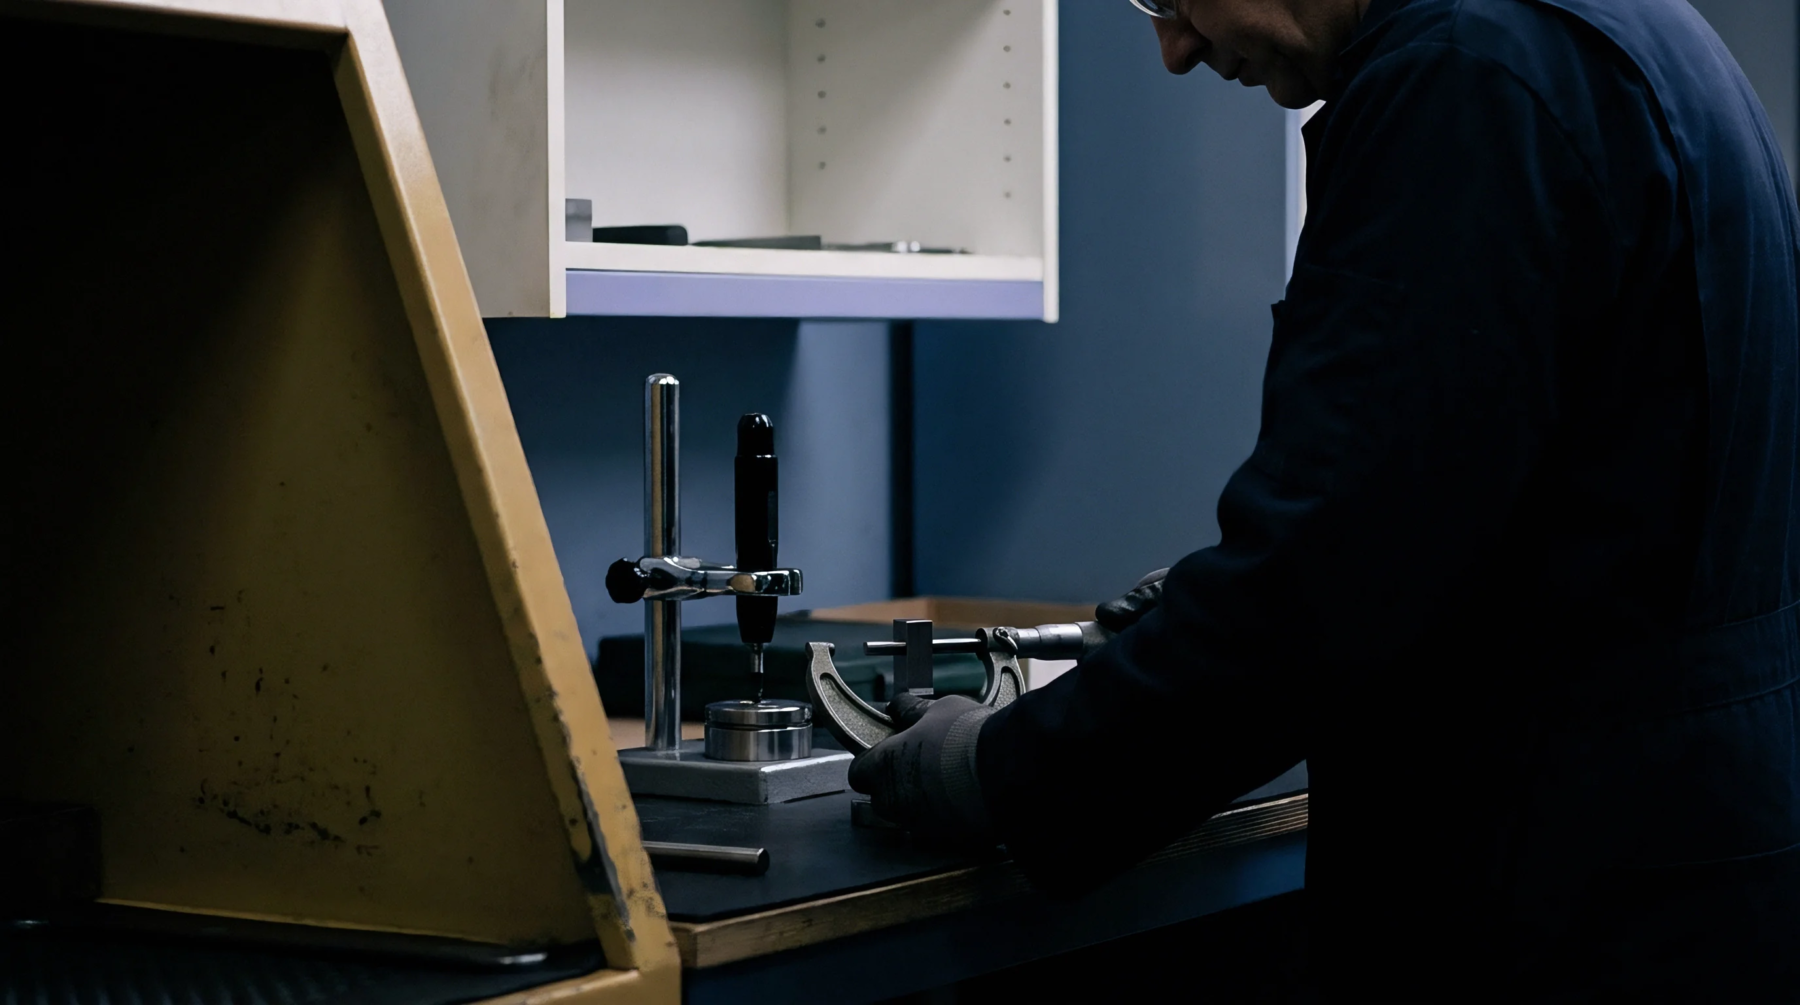
The physical displacement experienced by a workpiece under mechanical fixture pressure remains a critical variable in precision machining. Clamping deformation occurs when excessive holding force alters component geometry before the cutting tool engages the raw stock. Manufacturing engineers measure this dimensional shift during the initial tooling audit to verify fixture integrity.
Excessive displacement risks rejecting entire production lots once parts are released from the holding fixture and spring back to their unstressed state. Tooling designers must balance holding security against material yield limits to prevent permanent distortion. Boundary conditions apply strictly to elastic limits where removal of the fixture restores original dimensions without permanent plastic flow.
Operational Readiness
Plant managers evaluate fixture reliability through laser interferometry during the first article inspection run. Production lines halt immediately when metrology reports show dimensional drift exceeding established tolerances on thin walled castings. Calling fixture readiness early creates scrap rates that exceed ten percent of daily output because loose parts chatter under high feed rates.
Tooling teams often confuse theoretical holding capacity with actual holding capability under dynamic cutting loads. Dynamic cutting forces generate vibration harmonics that amplify holding displacement beyond static test bench predictions.
Thermal Variance
Heat generation from high speed milling softens metal alloys and reduces their resistance to fixture pressure. Coolant delivery systems mitigate thermal expansion gradients across the workpiece surface during heavy material removal cycles. Machine operators monitor spindle load monitors to detect binding caused by uneven thermal growth inside the hydraulic vice.
Temperature sensors embedded in the fixture base record thermal drift during extended production shifts. Thermal equilibrium determines whether the component cools inside the fixture or outside the containment zone.
Quality Verification
Coordinate measuring machines scan finished components after unclamping to verify geometric tolerance compliance. Dimensional data feeds directly into closed loop feedback systems that adjust subsequent fixture pressures automatically. Suppliers submit capability indices derived from batch sampling before receiving approval for volume manufacturing.
Metrology technicians separate mechanical displacement errors from thermal growth anomalies using differential sensor arrays. Fixture maintenance schedules depend on observed wear patterns rather than calendar intervals.